Introduction
The short answer is yes, AI vision sorting machines can operate with exceptional reliability in cold storage and frozen food environments—provided they are engineered with specialized thermodynamic and optical protections.
While standard optical sorters fail due to sub-zero temperatures, dense frost build-up, and lens condensation, next-generation AI vision sorting machines equipped with active climate-control cabinets, anti-fogging lens assemblies, and dynamic deep-learning algorithms can run continuously in these demanding conditions. At Easyweigh and Foodman, we design high-performance food sorting equipment that transforms cold-chain processing by maintaining high throughput, eliminating manual bottlenecks, and ensuring absolute quality compliance.
Challenges of Frozen Product Imaging
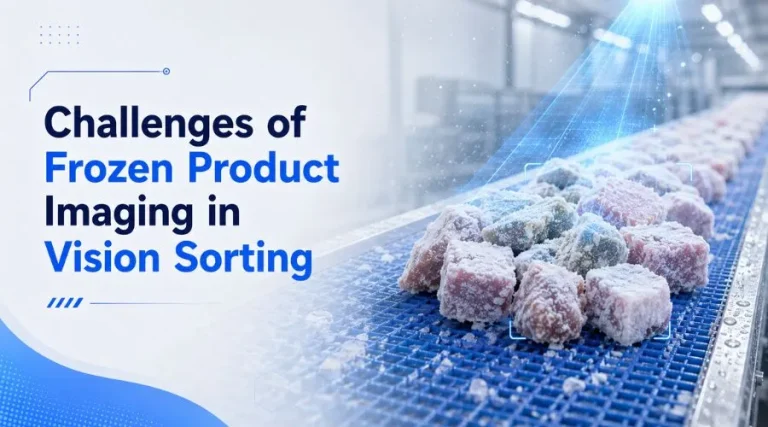
Operating a vision sorting machine or an optical sorting machine at temperatures below -18°C introduces severe optical and computational challenges that do not exist in ambient food processing. The primary obstacle is the physical transformation of the product itself. Frozen foods—such as individually quick-frozen (IQF) berries, vegetables, and seafood—are often covered in surface frost, ice glazes, or clustered together in frozen clumps.
The Problem of "Optical Occlusion" and Surface Frost
On a standard vegetable sorting machine or fruit sorting machine line, cameras rely on clean, unobstructed surfaces to detect defects like skin blemishes, rot, or foreign matter. However, in frozen lines, a layer of ice or frost scattering light acts as a visual shield. This “optical occlusion” causes a traditional optical sorter to misidentify harmless ice clusters as defects, or conversely, miss actual contaminants hidden beneath the frost.
Furthermore, when processing frozen seafood on a fish sorting machine or executing complex sorting and grading of fish, the surface water glaze creates highly reflective “hot spots.” This reflective glare blinds standard camera sensors. To overcome this, design vision sorting machine architectures must use multi-spectral and hyperspectral imaging. By combining short-wave infrared (SWIR) sensors with visible light cameras, an advanced optical sorter can look through the ice layer to detect the chemical signature of the underlying product, ensuring high-precision sorting fish and fish sorting accuracy.
Computational Challenges of IQF Clumping
Frozen products have a tendency to stick together, forming clumps as they travel down a conveyor. If a standard food sorting machine encounters a clump of three frozen strawberries, it evaluates them as a single, oversized, deformed object and rejects the entire cluster.
Next-generation optical sorting machines solve this through automated optical sorting software powered by deep-learning spatial segmentation. The AI vision sorting machines analyze the image not as a single silhouette, but as a composite of individual items. The software segments the clump, allowing the system to inspect each fruit within the cluster individually. This protects your yield and keeps your false reject rate close to zero.
Condensation and Lens Fogging Issues
In cold food processing, the most critical failure point for any vision sorting machine is condensation. When warm, humid air from the surrounding facility enters a cold machine, moisture instantly condenses on cold surfaces—particularly on camera lenses, LED illumination panels, and glass inspection windows.
The Physics of Dew Point in Cold Storage
Lenses that are even slightly fogged scatter light beams, making the camera blind. If a food sorting machine loses its visual clarity, its automated optical sorting accuracy drops immediately. The machine can no longer distinguish between a premium frozen pea and a piece of green plastic, forcing the line to stop for manual wiping.
To prevent lens fogging, Easyweigh engineers employ active thermodynamic barriers. Instead of using passive glass covers, our advanced technology keeps the glass temperature slightly above the ambient dew point, we prevent moisture from forming on the lens without affecting the frozen state of the product passing underneath.
High-Pressure Washdown and Thermal Shock
In frozen protein facilities, the daily cleanup routine poses a major risk of moisture ingress. Cleaning crews use high-pressure hot water (up to 80°C) to clean equipment that has been operating at sub-zero temperatures. This extreme temperature difference causes rapid metal contraction and expansion, known as thermal shock.
If a fish sorting machine or vegetable sorting machine lacks a properly sealed enclosure, this thermal contraction can pull humid air into the camera cabinet. Once the cabinet cools back down to sub-zero temperatures, that trapped humidity condenses inside the camera lens itself, causing permanent internal damage.
Hardware Adaptation for Cold Environments
Standard sorting machines are designed to operate between 0°C and 40°C. Running a reliable intelligent sorting system in these environments requires deep hardware adaptation. Pressurized and Heated Climate-Control EnclosuresTo protect the sensitive electronics inside our AI vision sorting machines, Easyweigh utilizes double-walled, insulated cabinets equipped with internal heating elements and pressurized air systems.
Pressurized and Heated Climate-Control Enclosures
To protect the sensitive electronics inside our AI vision sorting machines, we can utilize double-walled, insulated cabinets equipped with internal heating elements and pressurized air systems.
This positive pressure prevents moist external air from entering the cabinet, while the internal heaters keep the optical sensors, power supplies, and processors at their optimal operating temperatures. This climate-control system ensures the electronic sorting software runs smoothly without lag or thermal shut-downs.
Low-Temperature Pneumatics and Lubrication
At temperatures below freezing, standard pneumatic lubricants become thick and viscous, which slows down the response time of the ejector valves. If a valve experiences even a 2-millisecond delay, the air blast will miss the target defect and hit clean product instead, causing a spike in product loss.
To maintain consistent speed and accuracy in cold environments, Easyweigh sorting equipment uses specialized low-viscosity, food-grade synthetic lubricants and integrated air heaters within the pneumatic manifold. This ensures that the ejector valves fire with the exact same speed and power, whether the machine has been running for five minutes or five days.
How to Configure and Deploy an AI Vision Sorter in a Frozen Food Line?
To ensure your sorting line runs reliably with minimal downtime in cold environments, engineering and maintenance teams should follow this four-step setup and calibration process.
Step 1: Establish the Thermal and Pneumatic Baseline
Turn on the machine’s internal cabinet heaters and positive-pressure air systems at least 45 minutes before starting the product flow. Check the control panel to confirm that the internal camera enclosure has reached its stable operating temperature of 15°C to 20°C and that the pneumatic air line is dry and free of moisture.
Step 2: Calibrate for Frost and Reflective Glaze
Pass a sample run of frozen, frost-coated items through the scanning chamber. Use the software’s multi-spectral calibration tool to adjust the short-wave infrared (SWIR) sensors, setting the system to ignore surface frost and glare while highlighting the actual product structure underneath.
Step 3: Train the Neural Network on Segmenting Clumped Products
Pass a batch of clustered or clumped products through the optical sorter. Use the deep-learning segmentation tool to train the AI vision sorting machines to recognize individual items within a clump. This ensures the system grades each item accurately rather than rejecting the entire cluster.
Step 4: Verify Rejection Alignment and Pneumatic Speed
Run a mixed test batch containing both frozen products and known defects through the line at full production speed. Monitor the output to confirm the pneumatic ejectors are firing with the correct timing and pressure, adjusting the air manifold heater if you detect any valve lag.
Case Studies in Frozen Vegetable Sorting
High-Volume IQF Vegetable Processing
A major frozen vegetable processor in Europe faced high rates of product waste on their potato lines. Their traditional color optical sorter machine could not distinguish between a potato kernel covered in frost and a yellow plastic contaminant, leading to high rates of false rejects.
To address this, the plant installed an Easyweigh frozen vegetable sorting machine equipped with multi-spectral cameras and deep-learning software. The new system looked past the surface frost to evaluate the actual internal quality of each kernel. This upgrade reduced their false reject rate from 4.5% to under 0.3%, significantly improving their yield and delivering a fast return on investment.
Automated Seafood and Fish Grading
A large seafood processing plant in North America struggled with sorting frozen fish fillets. The reflective ice glaze on the frozen fish confused their existing sorting equipment, causing frequent errors during the sorting and grading of fish.
The facility upgraded their line with an Easyweigh marine-grade fish sorting machine featuring specialized reflective-glare filters and an IP69K washdown cabinet. The new setup allowed them to sort fish by dimension and grade with high accuracy, even with heavy ice glazes. The system streamlined their automated fish sorting and sorting of fish lines, helping them scale up their production capacity without adding manual labor.
System Reliability Considerations
When investing in an automated optical sorting system for cold storage or frozen food lines, choosing the right configuration is essential for securing long-term reliability and a fast payback period.
Comparative Analysis of Sorter Technologies in Cold Chain
To help you choose the right setup for your facility, this table compares different sorting technologies under cold-chain conditions:
| Feature / Metric | Traditional Color Sorter | Multi-Spectral Optical Sorter | Easyweigh AI Vision Sorter |
| Sub-Zero Temp Capability | Poor (No internal heaters) | Moderate (Requires external box) | Excellent (Built-in climate control) |
| Frost Penetration | None (Surface scanning only) | Moderate (SWIR sensors) | Excellent (SWIR + Deep Learning) |
| Condensation Protection | None (Frequent fogging) | Moderate (Passive air-purge) | Excellent (Heated windows + Pressure) |
| Clumped Product Handling | Poor (Rejects whole clumps) | Poor (Limited segmentation) | Excellent (AI Spatial Segmentation) |
| Washdown Protection | IP65 (Sensitive to moisture) | IP66 (Dust protected) | IP69K (High-pressure washdown safe) |
Long-Term Value and the Automated Sorter Market
As the global optical sorter market grows, food processors are moving away from basic, low-cost color sorters in favor of intelligent, durable sorting systems. While a specialized cold-chain optical sorting machine requires a higher initial investment, the long-term benefits are clear.
By eliminating condensation downtime, reducing false rejects, and preventing thermal shock damage, Easyweigh and Foodman systems deliver exceptional reliability. This high performance ensures consistent 24/7 operation in cold storage, protects your brand quality, and maximizes your plant’s profitability.
Summary: Main Takeaways for Cold-Chain Operators
Operating a successful frozen food line requires sorting systems designed to handle the physical and thermal challenges of cold environments.
Advanced Frost Penetration: Combining multi-spectral SWIR cameras with deep-learning software allows the system to look past surface frost and ice glazes, ensuring consistent accuracy on frozen lines.
Active Condensation Control: Using heated optical windows and positively pressurized camera enclosures prevents lens fogging, keeping your line running continuously without manual cleaning stops.
Durable Cold-Chain Hardware: Equipping machinery with internal heating systems and low-viscosity lubricants prevents component wear and valve lag, ensuring reliable operation in sub-zero cold rooms.
Intelligent Clump Segmentation: Utilizing spatial segmentation algorithms allows the system to inspect individual items within frozen clusters, protecting your yield and reducing waste.
FAQs
How does a Chinese AI sorting machine compare to European or Japanese brands in sorting accuracy?
Yes, an advanced optical sorter can run continuously in sub-zero environments, provided it features dedicated hardware insulation. Standard sorting machines encounter electronic lag and mechanical failures due to extreme cold. A specialized AI vision sorting machines setup solves this issue by using double-walled, heated, and pressurized climate-control cabinets. This insulation protects internal processors and sensors, allowing the electronic sorting software to function smoothly down to -18°C without component degradation.
How does optical sorting technology look past surface frost on a frozen vegetable sorting machine line?
Surface frost and ice crystals cause standard sorting machines to misidentify products because they scatter light beams and create visual blocks. A next-generation vegetable sorting machine or specialized food sorting machine addresses this by pairing Short-Wave Infrared (SWIR) sensors with visible light cameras. This optical sorting technology looks straight through the outer frost layer to evaluate the actual product structure underneath, allowing the food sorting equipment to separate true defects from harmless ice build-up.
Can an automated optical sorting line manage reflective ice glazes during fish sorting?
Yes. Processing maritime products via an automated fish sorting machine line introduces challenges from wet, highly reflective ice glazes that blind basic color sensors. A premium optical sorting machine engineered for the sorting of fish, sorting fish, or bulk fish sorting uses integrated hyperspectral arrays and polarizing filters. This setup eliminates reflective glare, allowing the intelligent sorting system to accurately handle the sorting and grading of fish by weight, length, and quality without dropping line velocities.